Why Is Color Stability a Key Benefit of White Short Fiber?
2026-09-20
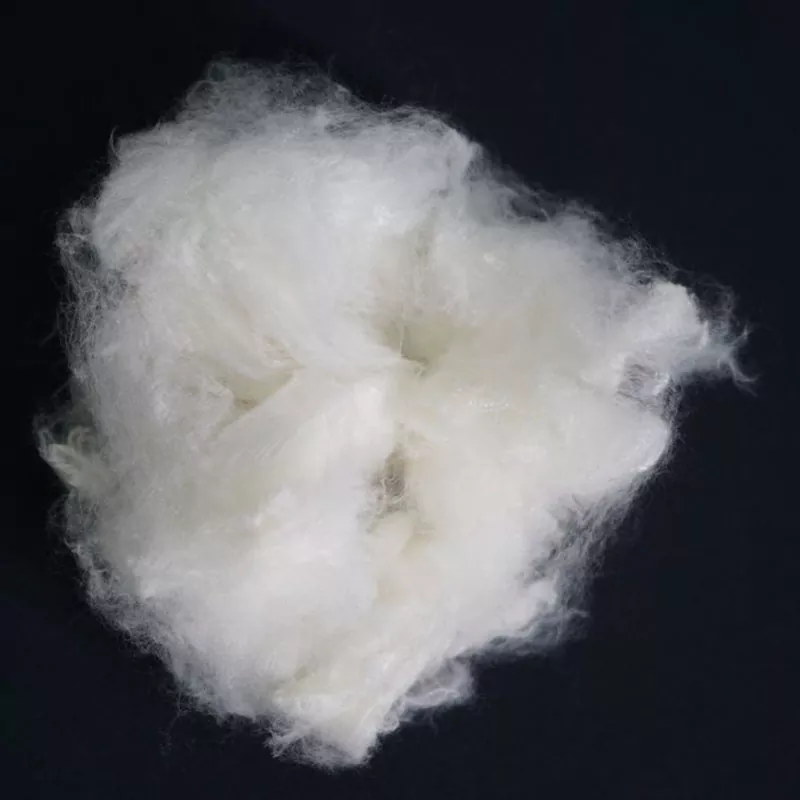
White Short Fiber is a foundational material in nonwovens, hygiene products, filtration media, and automotive interiors. In these applications, whiteness is not just an aesthetic preference—it is a functional requirement. A diaper that turns yellow on the shelf signals poor quality to the consumer. A filtration membrane that discolors indicates polymer degradation. An automotive headliner that fades unevenly creates a visible defect that leads to warranty claims. The ability of White Short Fiber to maintain its whiteness over time, under heat, and after UV exposure is what separates a premium material from a commodity one. This guide explains the science behind color stability and what to look for when sourcing.
1. What Causes White Short Fiber to Turn Yellow?
Yellowing in White Short Fiber is caused by three primary mechanisms: thermal oxidation, UV degradation, and chemical contamination. Thermal oxidation occurs when the polymer is exposed to elevated temperatures during processing or in the end-use environment. The heat breaks the polymer chains and creates conjugated double bonds that absorb blue light, making the material appear yellow. UV degradation occurs when ultraviolet radiation from sunlight breaks the chemical bonds in the polymer. This is a particular concern for outdoor applications such as geotextiles and agricultural covers. Chemical contamination can occur during production if the fiber comes into contact with oils, metal ions, or residues from processing equipment. Even trace amounts of iron or copper can catalyze yellowing reactions.
Yellowing chemistry: The yellowing of polyester and polypropylene fibers is primarily due to the formation of chromophores—chemical groups that absorb light in the blue region of the spectrum (400 to 500 nm). These chromophores are created by oxidation of the polymer chain. Antioxidants and UV stabilizers are added to the polymer to prevent this oxidation.
Inner Mongolia Fengshengtai New Material Co.,Ltd. has been producing White Short Fiber for over 15 years. Our factory controls the raw material specifications and the production process to minimize the formation of chromophores. We use virgin polymer with a controlled molecular weight distribution and add a proprietary antioxidant package that is optimized for the specific end-use application.
2. How Does Raw Material Selection Affect Color Stability?
The color stability of White Short Fiber begins with the raw material. Not all polyester or polypropylene chips are the same. The key parameters are the catalyst residue, the stabilizer content, and the molecular weight distribution. Catalyst residues, particularly antimony and titanium, can catalyze oxidation and lead to yellowing. Stabilizer content, including antioxidants and UV absorbers, determines the resistance to thermal and UV degradation. Molecular weight distribution affects the melt stability during fiber spinning. A narrow distribution with a high average molecular weight produces a more stable fiber. The table below shows the relationship between raw material parameters and color stability.
| Raw material parameter | Low stability | High stability | Impact on yellowness index |
| Catalyst residue (ppm) | > 50 | < 20 | High residue increases YI by 3 – 5 units |
| Antioxidant content (ppm) | < 500 | 1,000 – 1,500 | Higher content reduces YI by 4 – 6 units |
| UV stabilizer content (ppm) | 0 | 500 – 1,000 | Prevents UV-induced yellowing |
| Molecular weight (Mw) | Low (< 30,000) | High (> 45,000) | Higher Mw improves thermal stability |
| Moisture content (ppm) | > 200 | < 50 | Moisture causes hydrolysis during spinning |
Our factory sources polymer chips from suppliers who provide a certificate of analysis for each batch. We verify the catalyst residue, antioxidant content, and moisture content before accepting the material. This incoming inspection is the first line of defense against color instability.
3. What Production Process Controls Are Critical for Maintaining Whiteness?
The production process can either enhance or degrade the color stability of White Short Fiber. There are four critical control points. The first is the spinning temperature. If the polymer is heated above the optimal temperature, thermal degradation occurs. The second is the quenching rate. Rapid quenching produces a finer crystal structure, which is more resistant to yellowing. The third is the drawing ratio. A higher draw ratio aligns the polymer chains and increases the crystallinity, which improves stability. The fourth is the finish application. The finish (lubricant) must be compatible with the polymer and must not contain any yellowing precursors.
Process warning: A common mistake in fiber production is to increase the spinning temperature to improve throughput. This may increase output, but it also increases the yellowness index of the final fiber. The short-term gain in productivity is offset by the long-term loss in quality. Our factory maintains a strict temperature profile that is optimized for color stability, not just throughput.
The table below shows the effect of process parameters on the yellowness index of White Short Fiber.
| Process parameter | Typical range | Effect on yellowness index | Optimal setting for color |
| Spinning temperature | 280 – 300°C | +1 YI per 5°C above 290°C | 285 – 290°C |
| Quenching air temperature | 15 – 25°C | Lower temperature reduces YI | 18 – 20°C |
| Draw ratio | 3.0 – 4.5 | Higher ratio reduces YI | 4.0 – 4.5 |
| Finish concentration | 0.3 – 0.8% | Excess finish increases YI | 0.5% |
Inner Mongolia Fengshengtai New Material Co.,Ltd. monitors these parameters continuously during production. We use an online colorimeter to measure the yellowness index of the fiber every 30 minutes. If the YI exceeds the specification, the line is stopped and the process is adjusted. This real-time monitoring ensures that every batch meets the color stability requirement.
4. How Is Color Stability Verified and What Standards Apply?
Color stability is verified through accelerated aging tests that simulate the conditions of the end-use environment. The most common tests are heat aging, UV aging, and humidity aging. Heat aging is performed in an oven at 70°C to 100°C for 7 to 30 days. UV aging is performed in a QUV chamber with UVA-340 lamps for 100 to 500 hours. Humidity aging is performed in a humidity chamber at 40°C and 90% relative humidity. The yellowness index (YI) is measured before and after the test according to ASTM E313. A change in YI of less than 2 units is considered excellent. A change of 2 to 5 units is acceptable for most applications. A change of more than 5 units indicates poor color stability.
Test data from our factory: A batch of White Short Fiber with a starting YI of 2.1 was subjected to heat aging at 90°C for 14 days. The final YI was 3.4, a change of 1.3 units. The same fiber was subjected to QUV aging for 200 hours. The final YI was 4.2, a change of 2.1 units. These results meet the specification for hygiene and filtration applications.
Our factory provides a test report with every shipment of White Short Fiber. The report includes the initial YI, the YI after heat aging, and the YI after UV aging. This documentation allows our customers to verify the color stability of the material before it is used in production.
Frequently Asked Questions About Color Stability in White Short Fiber
Summary for Material Engineers and Procurement Managers
Color stability is a key benefit of White Short Fiber because it ensures that the final product meets the aesthetic and functional requirements of the application. Yellowing is caused by thermal oxidation, UV degradation, and chemical contamination. The raw material selection, the production process controls, and the verification testing all contribute to the color stability of the final fiber. When sourcing White Short Fiber, look for a supplier who provides full traceability, certificates of analysis, and accelerated aging test reports. Inner Mongolia Fengshengtai New Material Co.,Ltd. has been producing White Short Fiber for over 15 years and supplies to customers in the hygiene, filtration, and automotive industries.
Inner Mongolia Fengshengtai New Material Co.,Ltd. manufactures White Short Fiber with controlled yellowness index, high color stability, and consistent denier. We provide full test reports and technical support for all of our products.